The cost of getting compression timing wrong
Eventually reservoir pressure drops to the point where it can no longer push gas through the wells, gathering lines and processing inlet at the contracted delivery pressure. Past that point, rate falls faster than the reservoir alone would explain. The operator then faces two bad options. Compress too late and lose deliverable volume against a sales or domestic-supply commitment. Compress too early and pay capex, fuel gas and maintenance for pressure headroom the field does not need yet.
The squeeze is worst where reserves are shrinking and demand is fixed by contract or by domestic supply obligations, as in Bolivia's mature fields. There, decline is not really in question. The question is when the surface system becomes the binding constraint, and what that does to the remaining economically recoverable reserves. This article covers how to answer that with decline analysis and deliverability modelling, and how to turn the answer into a compression decision.
Standards and requirements context
Compression projects in late-life fields sit under several overlapping frameworks:
- PRMS (SPE Petroleum Resources Management System). It defines the economic limit as the time when maximum cumulative net cash flow occurs for a project (GeoExpro, Mature Fields: Easing into Retirement or a Second Career?). Any compression case that extends field life has to pass this test. Added opex pulls the economic limit earlier, even though it lowers abandonment pressure.
API 617covers axial and centrifugal compressors and expander-compressors for petroleum, chemical and gas industry services. It applies to central or subsea-class centrifugal machines.API 618covers reciprocating compressors for the same industries. It is the usual reference for larger reciprocating units. The packaged-unit standards from API and ISO apply to smaller wellsite packages.IEC 61511governs the functional safety of safety instrumented systems in the process industry. Compressor shutdown, anti-surge protection and high-pressure trips that tie into the field ESD fall under it.ISO 14224covers the collection and exchange of reliability and maintenance data. Use it to build a defensible availability assumption for the compression case, rather than leaning on vendor brochure figures.- The
IEC 60079series applies to equipment in explosive atmospheres. It governs area classification and equipment selection for wellsite and plant packages.
Decline forecasting: what it can and cannot tell you
Choosing the model
The standard empirical forms (Arps) are:
- Exponential: q = qi · exp(−D·t)
- Hyperbolic: q = qi / (1 + b·D·t)^(1/b), with 0 < b < 1
- Harmonic: the hyperbolic case with b = 1
You fit these to history, then extrapolate rate and cumulative production to an economic limit. A published decline-curve study of a Volve well shows the basic workflow. It projects economic lifetime to a stated end date, measured from a stated forecast date. The steps are fit, extrapolate to the limit, then read off remaining recoverable volume (Decline Curve Analysis for Forecasting Cumulative Production and Remaining Recoverable Volume in Well 15/9-F-12, Volve Field, 2026). The CED engineering primer makes the same point: every well, whether on primary, secondary or tertiary recovery, eventually declines.
Decline curves have a built-in weakness for compression planning. They extrapolate the past operating regime. A fitted trend reflects the backpressure the wells have actually seen. Once compression lowers wellhead pressure, the rate–time relationship changes, and the curve will not predict that change. It has no pressure variable in it.
Separating reserves from deliverability
Use two linked tools, each for what it does well.
- Material balance (p/z versus cumulative production Gp) estimates gas in place and how much reservoir pressure remains. For a volumetric gas reservoir:
p/z = (pi/zi) · (1 − Gp/G)
so recovery at any pressure is Gp = G · [1 − (p/z) / (pi/zi)].
- Deliverability (back-pressure) modelling relates rate to pressure drawdown:
q = C · (p̄r² − pwf²)^n
Here p̄r is average reservoir pressure, pwf is flowing bottomhole pressure, C is the performance coefficient and n is the deliverability exponent. Pwf is set by wellhead pressure plus tubing hydraulics. Wellhead pressure, in turn, is set by the gathering system and the delivery point.
The decline curve tells you what the wells have done. The pair above tells you what they can do at a different wellhead pressure. Compression timing is a deliverability question, and the decline curve is the cross-check.
Network-level scheduling
Compression rarely acts on one well. The framing still holds, though. Treat wells, gathering and compressor duty as one scheduling problem against a demand profile. Don't optimise them separately.
Locating the compression: a decision table
Location decides how much of the backpressure benefit reaches the reservoir, and what it costs to operate.
| Option | Where it acts | Main benefit | Main constraints | Source basis |
|---|---|---|---|---|
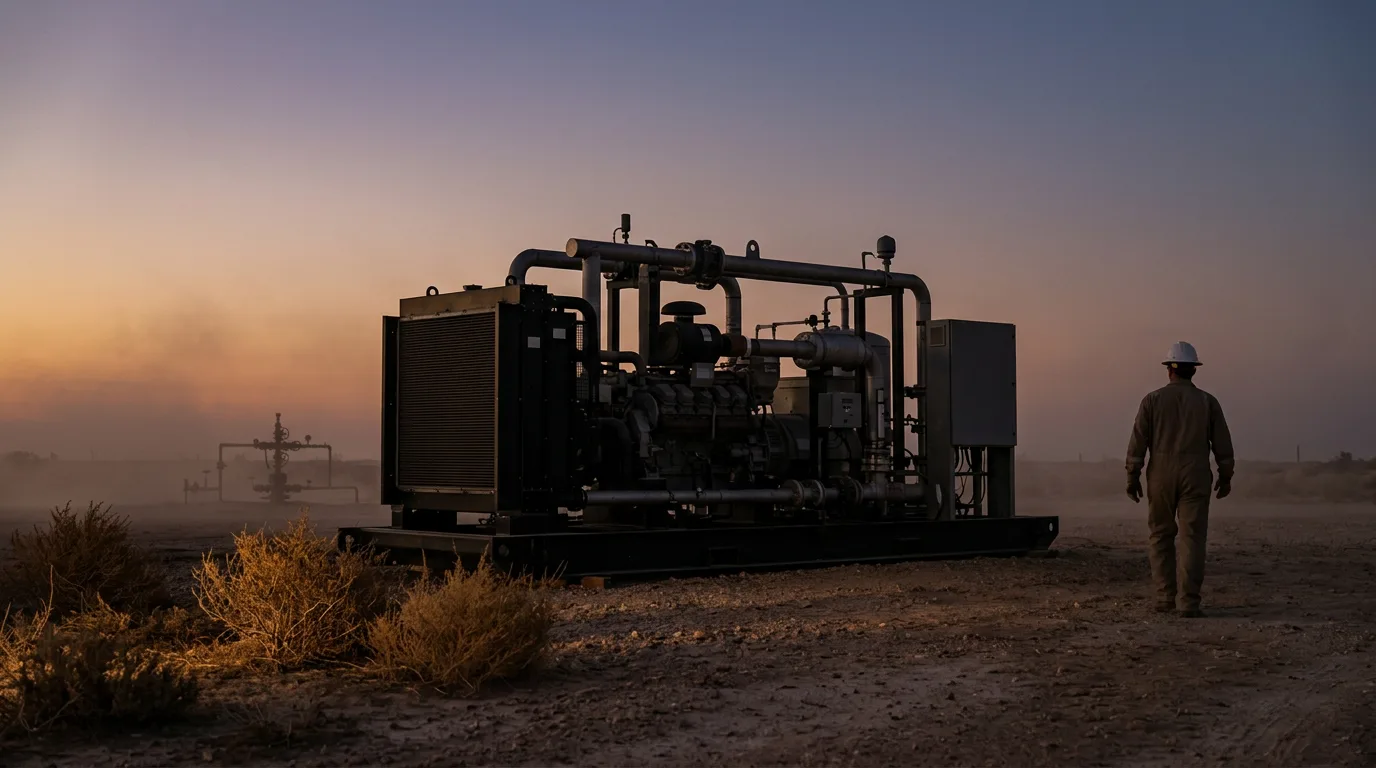
| Wellsite / wellhead compression | Individual wells or small clusters | Lowers wellhead pressure directly, so each well produces to a lower abandonment pressure | Many small units to maintain; fuel and power distribution; area classification at every site | PanCanadian wellsite programme (OSTI, 1998); SPE 182209 (2016) |
| Central field compression | Gathering inlet or plant | Fewer machines, easier maintenance and supervision | Gathering-line pressure drop limits the benefit to remote wells | Established practice |
| Subsea / remote compression | Seabed or far from the processing plant | Addresses long-tieback pressure loss | High intervention cost, qualification burden | Ormen Lange pilot (OTC, 2007) |
The planning rule is simple enough. If the pressure loss sits mainly in the flowline, moving compression toward the wells recovers the most. If the loss is in the reservoir and tubing, well-level boosting does most of the work.
The PanCanadian programme (OSTI, 1998) recovered additional gas from many wells using wellsite compressors. Both that programme and the table point the same way. For a large population of low-pressure wells, lowering wellhead pressure extends the productive life of infrastructure already in the ground.
Finding the timing trigger
Compression timing has two distinct drivers, and they point to different dates.
Rate-driven timing. This is the date when the field can no longer meet contract rate at the delivery pressure. Compression installed here defends plateau or contracted deliverability. The value comes from acceleration and from avoiding shortfall.
Reserve-driven timing. This is the date when compression is needed to push abandonment pressure lower and capture gas that would otherwise be stranded. The value comes from incremental recovery, and it can often wait. Reserves gained are largely independent of when the machine arrives, provided wells are not lost to liquid loading or water in the meantime.
Rate-driven timing usually comes first. Reserve-driven timing then sets how much compression capacity and turndown you need for the tail.
The IEA analysis of field decline rates is a useful reminder that decline is a portfolio-wide fact. It reviews the largest fields manually to find the timing and magnitude of peak production and the decline phases that follow. Treat decline as the base case and compression as a managed response to it.
Worked illustration: incremental recovery from lower abandonment pressure
Illustrative, symbolic. No field data are implied.
Take a volumetric dry-gas reservoir produced through a gathering system at fixed line pressure. The goal is to relate compression to extra recovery.
-
Define the abandonment condition. The well is abandoned when it can no longer deliver a minimum rate q_min. From the deliverability equation, set q = q_min: p̄r,ab² = pwf² + (q_min / C)^(1/n)
-
Link pwf to wellhead pressure. Tubing hydraulics give pwf as a function of wellhead pressure and rate. Compression lowers wellhead pressure, so pwf falls, and by step 1 p̄r,ab falls with it.
-
Convert to p/z. Evaluate z at each abandonment pressure to get (p/z)_ab,0 without compression and (p/z)_ab,c with compression.
-
Compute recovery in each case. Gp,0 = G · [1 − (p/z)_ab,0 / (pi/zi)] Gp,c = G · [1 − (p/z)_ab,c / (pi/zi)]
-
Take the difference. ΔGp = Gp,c − Gp,0 = G · [(p/z)_ab,0 − (p/z)_ab,c] / (pi/zi)
Result: Incremental recovery is proportional to gas in place and to the drop in abandonment p/z. A bigger drop, from lower wellhead pressure or better tubing hydraulics, gives more recovery. No claim is made about the size of ΔGp without field inputs.
How to use it. Run the calculation for each candidate wellhead pressure. Compare ΔGp with the discounted cost of the machine and its fuel. Then apply the PRMS economic-limit test. If compression opex pulls the cash-flow maximum forward, the extra recovery may not count as reserves in the PRMS sense.
Practical constraints that move the date
- Liquid loading. Lower wellhead pressure raises gas velocity at a given mass rate, which can help wells unload. Wells that are already loaded may need artificial lift as well.
- Gathering capacity. Compression raises volumetric flow in lines sized for higher pressure. Check velocity and erosion limits, and confirm that downstream separation and dehydration can take the extra volume.
- De-bottlenecking first. Removing surface restrictions can defer compression, and it improves the economics when compression does arrive.
- Modularity and redeployment. Wellsite packages can be moved as wells decline. That suits a tail-end profile better than one large machine sized for the peak.
Safety during tie-in and maintenance
Compressor tie-ins, filter changes and pipework modifications open hydrocarbon-containing equipment. The work plan must cover:
- Positive isolation by closed valves and spades or blinds.
- Controlled depressurisation to a safe location.
- Verification of zero energy by gauges and a bleed check at the lowest point.
- Lock-out/tag-out of all energy sources, including starter, power and instrument gas.
- Hazardous-area precautions in line with the site classification, using certified tools and equipment.
- Continuous gas detection at the work area.
- Venting or flaring to a safe, approved location, with purging before any hot work.
Checklist for the compression decision
- Fit decline curves to history, and flag the date of any backpressure change that breaks the trend.
- Build a p/z material balance and test it against pressure surveys before using it to set abandonment targets.
- Construct well deliverability curves and coupled tubing and gathering models to find the date when contracted rate cannot be met.
- Separate rate-driven from reserve-driven timing and assign each a date range.
- Compare wellsite, central and remote options on where the pressure loss actually sits.
- Complete de-bottlenecking and well optimisation before committing capex.
- Check liquid-loading behaviour at lower wellhead pressure.
- Test the PRMS economic limit with compression opex included.
- Define reliability and availability assumptions from your own site data, structured per
ISO 14224. - Confirm the machine standard (
API 617orAPI 618), the safety instrumented function design underIEC 61511, and area classification underIEC 60079before issuing the enquiry. - Plan for redeployment or turndown in the tail.
Conclusion
Compression timing is set by the deliverability model, with decline curves as the check. Establish the date when the system fails contracted rate, then the pressure at which wells fail minimum rate, and use those two dates to size and phase the machines. Start by building the coupled well-and-gathering deliverability model and running the incremental-recovery calculation at several wellhead pressures. Rank wellsite, central and remote options against the results. Issue the equipment enquiry only after the economic-limit test has been passed with realistic compression opex.