Why LPG and NGL custody transfer punishes poor meter selection
Light hydrocarbons run close to their bubble point, and that leaves very little room. A Coriolis meter sized only on flow rate can still drop enough pressure across its tubes to flash product inside them. Once vapour forms, the density and mass readings both go bad, and the transmitter may keep showing a steady but wrong total. On a fiscal loading or pipeline delivery, that bias goes straight onto the invoice and into the imbalance reconciliation. Then the dispute lands on the instrument engineer's desk.
Zero stability, installation stress and proving cause the same kind of trouble. A meter picked for its headline accuracy can still fail a fiscal audit. The low end of its range may be dominated by zero instability, or the prover connections may never have been designed for a pressurised, volatile fluid. This guide covers sizing logic, installation effects and proving for LPG and NGL, so the selection holds up under audit.
Standards and requirements context
For liquid hydrocarbons, the framework is mostly API and OIML:
API MPMS Chapter 5.6covers measurement of liquid hydrocarbons by Coriolis meters. It is the primary reference for fiscal use.API MPMS Chapter 4covers proving systems.API MPMS Chapter 4.5covers master-meter provers.API MPMS Chapter 11.2.4covers temperature correction for the volume of NGL and LPG. It matters when the contract settles in volume at reference conditions, even though the meter measures mass.OIML R 117covers dynamic measuring systems for liquids other than water. It applies where legal metrology approval governs the installation.ISO 10790gives guidance on selection, installation and use of Coriolis meters.- The
IEC 60079series governs equipment in explosive atmospheres. It applies to the sensor, transmitter and any junction boxes.
Treat this as the performance envelope your contract and regulator will expect. Your measurement uncertainty budget and the weights-and-measures authority set the actual acceptance criteria.
Sizing starts from the mass flow range, but for LPG and NGL three constraints interact.
Step 1: Define the operating envelope in mass units
Convert your volumetric loading or pipeline rates to mass flow, because Coriolis ranges are specified in mass:
ṁ = Q × ρ
where ṁ is mass flow (kg/h), Q is volumetric flow (m³/h) and ρ is flowing density (kg/m³). Use the density at the lightest, warmest, lowest-density product case for the maximum volumetric rate, and the heaviest, coldest case for the minimum. LPG density swings with composition and temperature. A meter sized on a single propane figure can end up mis-ranged the first time it sees butane or a mixed product.
The manufacturer's sizing software, run with the actual product properties, must close the selection.
Step 2: Check pressure drop against vapour pressure
Pressure drop across the meter rises with flow. The lowest pressure inside the sensor occurs at maximum flow and highest temperature. Your check is:
P_downstream − ΔP_meter must remain above the product's vapour pressure at flowing temperature, with a margin.
Take the vapour pressure from the product specification or an equation of state at the highest expected temperature, not from a nominal value. Your measurement or process-safety philosophy should set the margin, since it has to cover transients, valve behaviour and composition changes. If the check fails, you have three options:
- Select a larger meter, accepting poorer low-flow performance.
- Raise back pressure by relocating or re-tuning the control valve.
- Use parallel meter runs.
Do not accept a selection that passes only at nominal conditions.
Step 3: Check low-flow uncertainty from zero stability
Each Coriolis meter has a zero-stability specification in mass flow units. Its contribution to uncertainty grows as flow falls:
Zero-stability error (% of reading) = (zero stability ÷ actual mass flow) × 100
Evaluate this at your minimum operating flow, such as the start of a loading ramp or a low pipeline turndown. If it takes too large a share of the uncertainty budget, the meter is oversized. This is the usual clash with Step 2. A smaller meter helps zero stability, while a larger one helps pressure drop. Resolving it often means running two meters in parallel with staging, rather than compromising on one.
Selection comparison
| Criterion | Why it matters for LPG/NGL | What to verify |
|---|---|---|
| Pressure drop at max flow | Flashing causes density and mass errors | Calculated with product viscosity and density at worst-case conditions |
| Zero stability | Dominates uncertainty at low flow | Manufacturer's value against minimum flow in your uncertainty budget |
| Pressure rating | Vapour pressure and surge conditions | Sensor and flanges rated for maximum credible pressure |
| Density accuracy | Supports volume derivation and composition checks | Density calibration certificate and its reference fluid |
| Approvals | Fiscal acceptance | Legal-metrology or regulator approval where required, plus hazardous-area certification |
| Sensor geometry | Vapour release and drainability | Orientation guidance from the manufacturer for liquids that can flash |
Configuration matters as much as the sensor. Cutoffs, damping and density settings can move the reported total just as much as the choice of sensor does.
Installation effects that bias fiscal results
Coriolis meters are not very sensitive to upstream flow profile, which is why their straight-run requirements are modest. They are far more sensitive to the following.
Vapour and pressure control
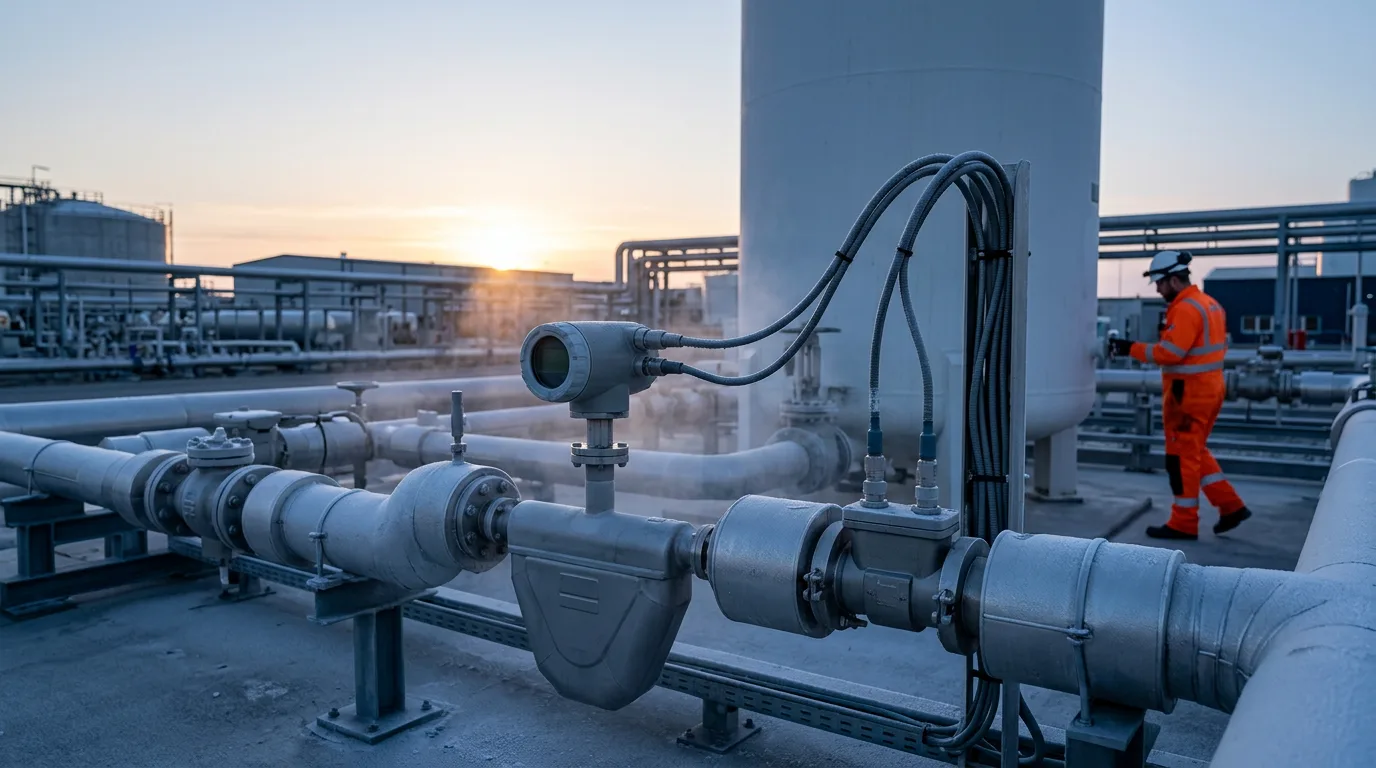
- Place the flow control valve downstream of the meter so the meter sits at the highest available pressure.
- Fit a vapour or air eliminator upstream where loading arms, pump suction or tank-bottom conditions can let gas in.
- Keep pump cavitation sources out of the immediate upstream run.
Mechanical stress and vibration
- Support the piping so the sensor sees no pipe strain, bending or torque. Misaligned flanges are a common cause of zero shift.
- Keep the sensor away from pump pulsation and strong vibration sources. Separate adjacent meters as the manufacturer instructs to avoid cross-talk.
Thermal behaviour
- Place the temperature transmitter close to the meter. The pressure transmitter should sit at a representative tapping, because both feed density and volume correction.
- Fit thermal relief on any section of LPG or NGL pipework that can be blocked in between isolation valves. Liquid expansion can overpressure the section, and it does so faster than most people expect.
Orientation and zeroing provisions
- Orient the sensor per the manufacturer's guidance for liquids that can release vapour, so the tubes stay liquid-full and any gas drains clear.
- Provide double block and bleed isolation upstream and downstream. That lets you zero the meter full of product, at line pressure and temperature, with no flow.
Proving requirements for fiscal service
Fiscal installations normally prove the meter in situ against a reference. The reference may be a pipe or compact prover, a master meter or a gravimetric method. API MPMS Chapter 4 sets the framework. API MPMS Chapter 5.6 covers Coriolis-specific points such as when to zero and how to apply a meter factor.
Practical points:
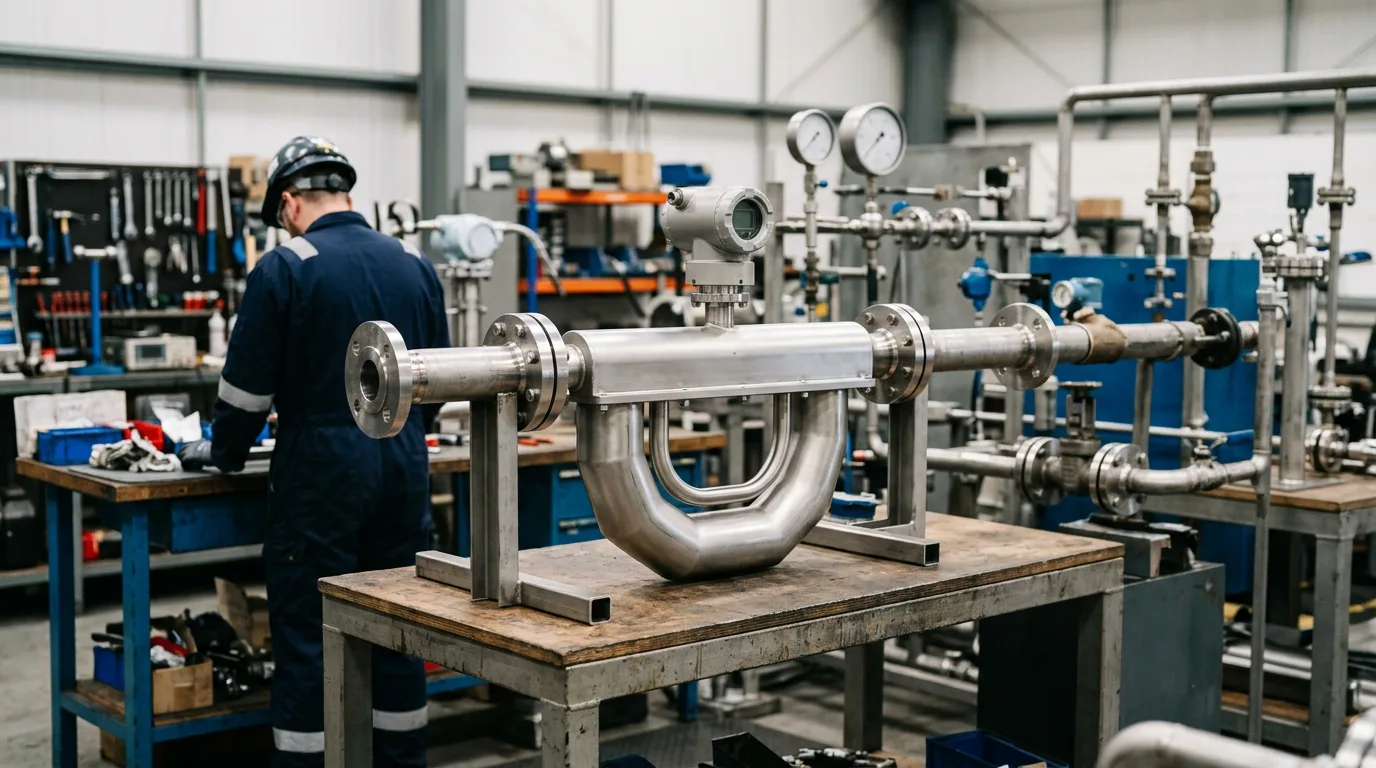
- Pressurised provers. LPG and NGL provers must hold product above vapour pressure. Prover connection design, vent routes and drain routes need settling at the design stage, not after the first proof fails.
- Master meters. Liquid Gas UK User Information Sheet 09, Selection and Operation of Coriolis Meters for Proving LPG Metering Equipment by Volume, records that Coriolis meters are widely used for checking LPG metering equipment. The same discipline applies when your Coriolis meter is the device under test. The reference and the meter must see the same product at the same conditions.
- Order of operations. Zero the meter under verified no-flow, full-pipe conditions before the proving run. Record the zero value and the meter factor together, so a shift in one can be traced against the other.
- Trending. Keep a meter-factor control chart. A drifting factor, a moving zero or a gap between measured and expected density points to fouling, damage or a pressure-control problem, and it does so long before a single proof fails.
- Density as a diagnostic. Compare reported density against the laboratory or composition-derived density from the sample. A persistent difference points to a calibration, vapour or sampling issue.
Safety during zeroing, proving and sensor access
Any work that opens or inspects LPG or NGL equipment, including breaking prover connections or removing a sensor, needs a permit-controlled sequence:
- Isolate the meter run with the double block and bleed arrangement.
- Depressurise to the closed drain, flare or recovery system. Never vent to atmosphere.
- Verify zero energy by confirming zero pressure at the bleed and checking that the bleed stays clear.
- Apply lock-out/tag-out to the isolation valves and to the pumps and control valves that could repressurise the section.
- Purge or inert as the site procedure requires, and use calibrated portable gas detection before and during breaking containment.
- Use only tools and test equipment certified for the hazardous area classification.
- Re-establish containment, leak-test and bring the section back up slowly, so the sensor is not hit by a flashing front.
Illustrative scenario: selecting for a mixed-product loading gantry
This is a qualitative scenario for guidance, not a completed sizing calculation.
A terminal loads propane and butane to road tankers. The design question is whether one large meter or two smaller meters in parallel should serve each bay.
- Convert the maximum loading rate and the slow-start rate to mass flow, using the lightest and heaviest product densities respectively (Step 1).
- Obtain the product's vapour pressure at the highest expected summer temperature, and the lowest available pressure at the loading arm.
- Using the manufacturer's pressure-drop curve for the candidate size, check that the lowest sensor pressure stays above vapour pressure with margin. If the single large meter passes only with the control valve almost fully open, the design has no operating margin.
- Calculate the zero-stability contribution at the slow-start rate. If the single meter doesn't fit within the uncertainty budget at that rate, either specify two meters with the second staged in at higher flow, or restrict fiscal totalisation to flow above a defined minimum, agreed with the counterparty.
- Confirm there is a route for a prover or master meter connection and a defined proving frequency.
In most cases like this, the pressure-drop check against vapour pressure, rather than the accuracy specification, decides the meter size.
Selection and commissioning checklist
- Mass flow range defined from real product density cases, not a single nominal value.
- Vapour pressure taken at the highest flowing temperature, with a stated margin to the lowest sensor pressure.
- Pressure drop verified at maximum flow using the manufacturer's sizing tool.
- Zero-stability contribution calculated at minimum flow and included in the uncertainty budget.
- Control valve located downstream of the meter; vapour eliminator provided where gas can enter.
- Pipe supports checked for zero strain; vibration and neighbouring meters assessed.
- Thermal relief provided on every blockable liquid section.
- Pressure and temperature transmitters located for representative density and volume correction.
- Double block and bleed provided for zeroing and proving, with a closed drain or recovery route.
- Prover or master-meter connections designed for pressurised volatile product.
- Legal-metrology approval, hazardous-area certification and calibration certificates on file.
- Zero value, meter factor and density comparison recorded at commissioning as the baseline for trending.
Conclusion
For LPG and NGL, pressure drop against vapour pressure and zero stability at minimum flow decide the meter size. Accuracy claims come second. Build the selection on mass flow cases from real product densities, close each constraint with the manufacturer's sizing software, and design the zeroing and proving provisions into the piping from the start.
Your next steps are to run the vapour-pressure margin check on your current or planned meters, confirm the proving route against API MPMS Chapter 4 and API MPMS Chapter 5.6, and start a meter-factor and zero trend so that drift shows up before it becomes a fiscal dispute.