Ex equipment leaves commissioning with a clean file and then deteriorates. Corrosion sets in, seals degrade, cables get damaged, covers go back on with missing fasteners, and field modifications are made that no one records. Most sites have a periodic inspection programme, but it often fails in one of two ways. Either it is a visual walk-round that is called "periodic" and never goes deeper, or every item is scheduled for detailed inspection, which the plant cannot resource, so a backlog builds and the records become unreliable. Both leave ignition sources in classified areas and both look poor in an audit.
This article separates what IEC 60079-17 asks for from common habits, and ends with a condition-rating template you can adapt on site.
Standards context
IEC 60079-17 (Explosive atmospheres – Part 17: Electrical installations – inspection and maintenance) defines inspection and maintenance of electrical installations in explosive atmospheres. It sits alongside three other standards:
- IEC 60079-14 covers design, selection and erection of electrical installations.
- IEC 60079-10-1 covers classification of areas with explosive gas atmospheres.
- IEC 60079-19 covers equipment repair, overhaul and reclamation.
The standard defines the method: grades of inspection, types of inspection, competence and documentation. It does not rank your defects or decide your priorities, so a site rating scheme is still needed. National law may add its own duties. For example, the Hungarian source used here notes that Decree 3/2003 obliges the operator to ensure proper maintenance and inspection of Ex equipment, and that authorities and insurers refer to IEC 60079-17 for the method.
The three grades: depth of inspection
The grades describe how deep an inspection goes. They are cumulative, and each one includes the one before it.
| Grade | What it finds | Access and tools | Typical examples |
|---|---|---|---|
| Visual | Defects apparent to the eye | No access equipment or tools | Missing bolts, damaged enclosure, absent or illegible marking, missing blanking element |
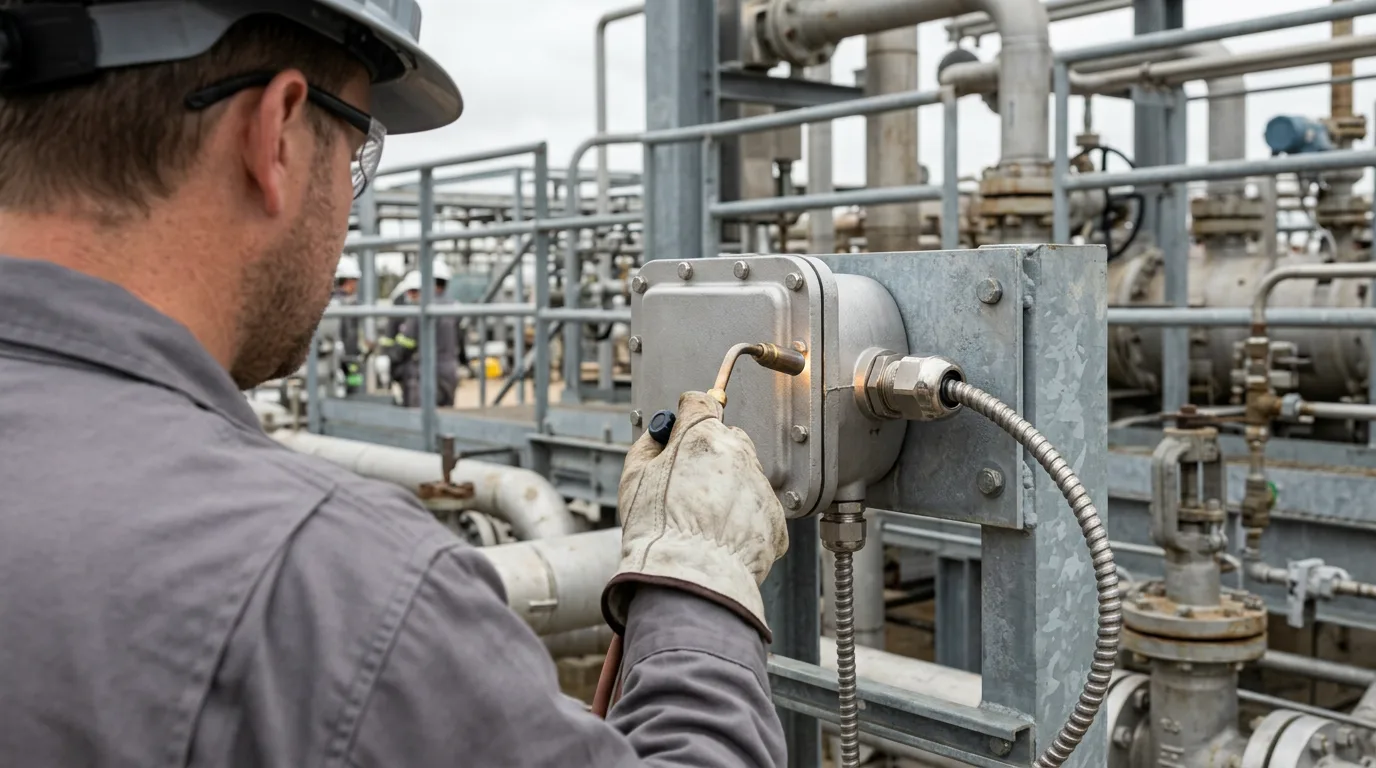
| Close | Everything visual finds, plus defects needing access or tools | Steps or tools may be needed. The enclosure is not normally opened and equipment is not de-energised | Loose bolts, loose or damaged glands, cable entry condition, condition of supports |
| Detailed | Everything close finds, plus defects visible only inside | Enclosure opened and/or test equipment used, which normally means isolation | Loose terminations, internal condition, seals, flamepath condition, insulation and earth checks |
The common mistake is treating "close" as the default for everything. A close inspection cannot find a loose termination inside an increased-safety terminal box, so it does not replace a detailed inspection on a risk-based sample or at initial inspection. Equally, scheduling every item for detailed inspection means opening enclosures that did not need opening, and each opening adds its own risk of damaged seals, contamination and wrongly reassembled covers.
The three types: when and why
The type of inspection answers why you are inspecting. The grade answers how deep.
| Type | Purpose | Grade | Trigger |
|---|---|---|---|
| Initial | Confirm the equipment and installation are suitable before service | Detailed | New installation, or equipment or classification change |
| Periodic | Confirm continuing suitability as the equipment ages | Visual or close, with detailed where the inspection plan requires | Scheduled interval |
| Sample | Test whether the lower-grade periodic regime is hiding deeper faults | Higher grade applied to a representative subset | Part of the periodic plan, extended if faults are found |
That works only where those personnel are frequently on site, trained in Ex, and their observations are recorded and acted on. A general operator round with no Ex training does not meet that description.
Where field practice departs from the standard
Skipping or diluting the initial inspection
The manufacturer's certificate and a factory test report prove the equipment type. They do not prove that the installation is correct. Wrong glands, unsealed entries, incorrect cable types and altered earthing are installation faults, and only a detailed initial inspection finds them. If initial inspection is skipped, every periodic inspection that follows rests on an unverified baseline.
"Periodic" meaning a visual walk-round
A visual round is a useful grade. As the only grade it leaves out entire fault classes, such as loose terminations, degraded seals and internal condition. The periodic plan should state, per equipment group, which grade is applied each cycle and which grade is applied on the sample.
Sampling without a sampling logic
A sample is only credible if it is representative. A sensible sample covers each protection concept, each area type, and the harsher environments (outdoor, corrosive, vibrating, heavily washed down). It should include equipment that is heavily used or often opened. The plan should say in advance what happens if the sample finds faults: widen the sample, and in the worst case inspect the whole group at the higher grade. A sample that never grows regardless of findings is a way of avoiding work.
One interval for everything
Many sites run a single site-wide cycle because it is simple to schedule. The standard expects the interval to reflect the equipment type, its environment and exposure to corrosion, weather and vibration, the manufacturer's guidance, and what past inspections found on similar equipment. Intervals should be reviewed against inspection results. Where a group repeatedly shows deterioration, shorten its interval. Where results are consistently clean, lengthen it, with a documented rationale and, where the standard's guidance on maximum intervals applies, expert advice.
Intrinsic safety treated as a tick-box
A LinkedIn discussion by Kannan N asks directly whether periodic inspections really verify intrinsic safety. The point is a fair one. The standard requires checks that diode safety barriers, galvanic isolators, relays and other energy-limiting devices are of the certified type and installed as the certification requires. In practice inspectors often confirm only that a barrier is present and tagged. Verifying an intrinsically safe loop means comparing the loop against its documentation: the certified parameters of the apparatus, cable parameters, earthing arrangement of barriers, and segregation of IS and non-IS circuits. If the loop documentation is missing or out of date, record that as a finding. It is not a reason to skip the check.
Competence assumed rather than demonstrated
The periodic-inspection personnel clause in IEC 60079-17 asks for people who understand area classification and equipment protection level (EPL) well enough to see what they mean for the location. They must also know the protection concepts, the installation practice and the relevant standards. Fabrico's guide stresses documented competence as a core requirement. Keep a competence record per inspector, and do not let a general electrician sign off Ex inspections on the strength of general electrical experience.
Records that cannot prove anything
A defensible record has three parts:
- An equipment register that identifies each item, its location, its zone and EPL, and its certification.
- An inspection record that shows type, grade, date, inspector and findings for each item.
- A defect and closure record that shows who corrected what, and when.
The Hungarian source recommends photo-documented reports, which also help when a finding is disputed later. A register that is not reconciled with the area classification drawings, or that ignores modifications, will contradict the field.
A condition-rating template
The standard does not give a defect-priority scheme. Keep one on site, but do not confuse its terms with the inspection grades. The scheme below uses "rating" for condition, and you should adapt the examples and response wording to your permit system and risk matrix.
| Rating | Definition | Example findings | Required response |
|---|---|---|---|
| A – Compliant | No deviation from certification or installation requirements | Fasteners complete, entries sealed, marking legible | Record and continue the cycle |
| B – Minor | Deviation with no loss of protection concept | Faded marking, light surface corrosion, paint damage away from flamepaths | Schedule correction in routine maintenance. Track to closure |
| C – Major | Protection concept degraded or in doubt | Loose terminations, damaged or incorrect gland, missing fasteners on a flameproof cover, unverified IS loop documentation | Remove from service or make safe by isolation until corrected. Raise a defect with an owner |
| D – Critical | Protection concept absent or equipment clearly unsuitable | Missing cover, uncertified replacement, wrong EPL for the zone, open entry, damaged flamepath | Isolate immediately and tag out. Investigate cause and extent. Review the sample |
Record the following alongside each rating:
- Equipment tag.
- Zone and EPL.
- Inspection type and grade.
- Rating.
- Defect description with photograph.
- Corrective action and owner.
- Closure date and verifier.
Make a decision rule for the sample: any C or D rating in a sampled group triggers an extension of the sample for that group. Name who may close the trigger, and require written justification when it is closed without extension.
Illustrative scenario
This scenario is illustrative, not a real event. A gas processing module has a population of increased-safety terminal boxes of the same type, installed outdoors in a washed-down area. The previous cycle was visual only, and every box was rated A.
The new plan keeps visual grade for all boxes and adds a sample at detailed grade covering several boxes, selected from the most exposed positions and from boxes that maintenance opens most often. During the sample, several of the opened boxes show loose terminations and degraded cover seals. Under the decision rule, these C ratings extend the sample to the whole group. The wider inspection finds the same fault pattern in the more exposed locations, so the interval for that group is shortened and the sealing specification is revised.
None of those faults was visible at visual grade. The earlier A ratings were accurate for what had been inspected and misleading for what had not.
Safety precautions for detailed inspection
Detailed inspection usually means opening enclosures in or near classified areas. Before opening any enclosure:
- Confirm the permit covers the work and the area classification.
- Isolate the circuit at its source, apply lockout/tagout, and prove the circuit dead with a tester that has itself been proven.
- Verify zero stored energy, including capacitors, back-fed supplies and other circuits entering the enclosure.
- Gas-test the immediate area before opening, and continue monitoring where conditions can change. If adjacent process equipment is under repair or breakdown, confirm that the area is safe from vented or purged hydrocarbons and that nothing is venting nearby.
- Do not open an enclosure that is not isolated unless it is certified for it and the permit allows it.
- For pressurised (purged) enclosures, follow the purge and re-pressurisation sequence before re-energising.
- Use test instruments suitable for the area, or work under a permit that allows non-certified instruments.
- On reassembly, inspect flamepaths, gaskets and seals, refit all fasteners to the specified type, and record the work.
Practical checklist
- Is there an equipment register that matches the area classification drawings and records EPL and certification for each item?
- Has every item had a recorded detailed initial inspection?
- Does the plan state the grade for each equipment group, each cycle?
- Is the sampling basis documented, including what extends the sample?
- Is each interval justified by equipment type, environment and past findings, and reviewed against inspection results?
- Are IS loops checked against certified parameters and loop documentation, not just for the presence of a barrier?
- Does each inspector have a competence record covering classification, EPL and protection concepts?
- Is there a condition-rating scheme with defined responses and named owners?
- Do records include photographs, defect closure and verification?
- Is there a link between modification control and the register?
- Is isolation, LOTO and gas testing documented for every detailed inspection?
Conclusion
IEC 60079-17 does not ask for the deepest inspection on every item. It asks for the right grade, for the right reason, by competent people, with records that show what was done. Start by reconciling your register with the classification drawings. Then write down your grade-by-group plan and sampling rules, adopt the condition-rating scheme in this article (adjusted to your risk matrix), and test it on one area before rolling it out. The first detailed sample will tell you quickly whether your existing ratings can be trusted.